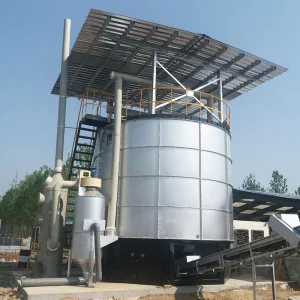
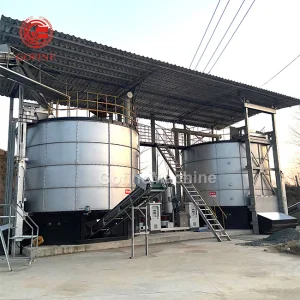
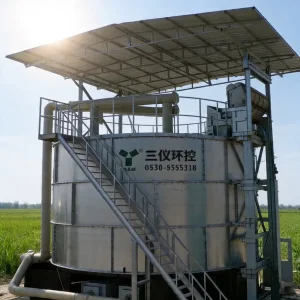
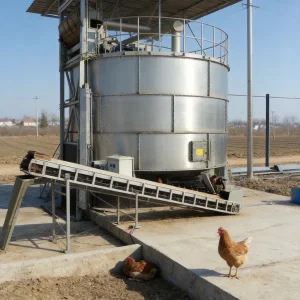
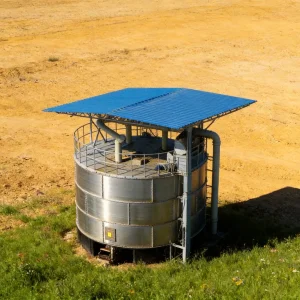
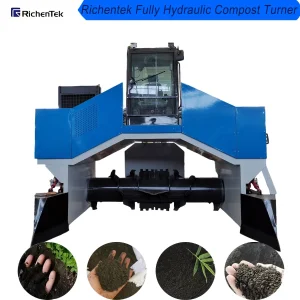
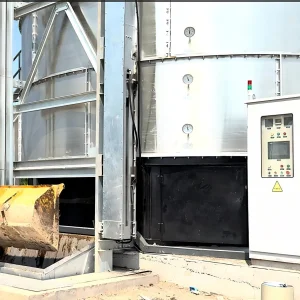
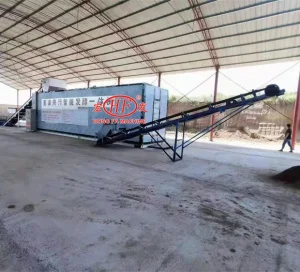
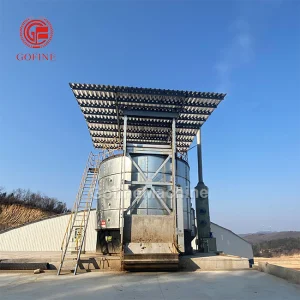
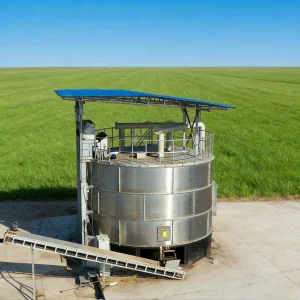
Discover our core industrial composting machines engineered to convert raw poultry waste into high-grade, pathogen-free organic fertilizer for local agricultural optimization.
Skopje, as the political and economic hub of North Macedonia, sustains a robust agricultural framework characterized by intense livestock farming, poultry breeding, and sprawling horticultural operations in the surrounding Vardar valley. However, rapid commercial expansion brings acute environmental challenges. Traditional poultry farming generates massive volumes of high-nitrogen manure, which—if left untreated—poses severe threats to local groundwater tables through nitrate leaching and contributes heavily to regional ammonia emissions.
Local agricultural producers and municipal environmental agencies in Skopje are shifting rapidly toward circular economy models. Regulatory frameworks aligned with European environmental standards demand strict controls over agricultural runoff and organic waste disposal. Consequently, implementing high-efficiency Poultry Waste Composting Machines is no longer optional; it is an industrial necessity for modern poultry operations aiming for long-term viability, biosecurity compliance, and value recovery.
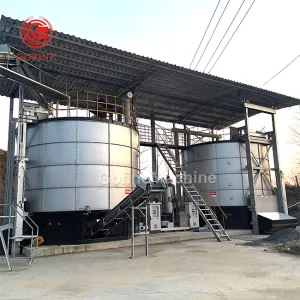
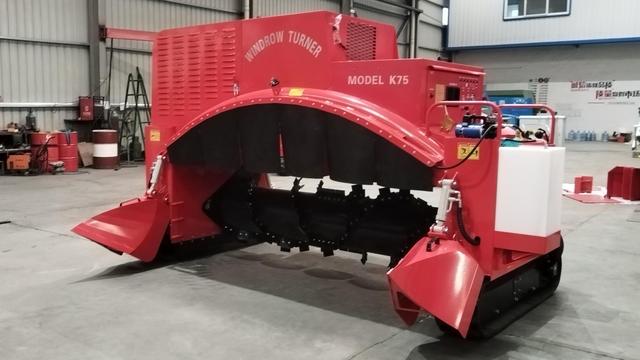
Globally, the paradigm of animal husbandry has shifted from sheer volume production to sustainable, zero-waste bio-security ecosystems. Chengdu AgBio Energy Co., Ltd. stands at the forefront of this industrial revolution. By integrating automated thermophilic aerobic fermentation, our systems accelerate organic decomposition from months to mere days, locking in vital nutrients while eliminating weed seeds, insect larvae, and harmful pathogens.
Our macro-level engineering approach accommodates diverse operational scales—from medium-sized independent poultry farms in the Balkan region to large-scale municipal organic waste processing plants. Through integrated odor control scrubbers, automated moisture sensors, and intelligent PLC control panels, our composting infrastructure guarantees clean, odor-free, and energy-efficient operations suitable for proximity to urban residential zones in Skopje.
Tailored deployment strategies ensuring seamless integration into Skopje’s agricultural landscape.
1. Commercial Poultry Breeding Complexes: Immediate inline processing of daily cage manure, drastically reducing fly infestation and foul odors on-site.
2. Agricultural Cooperatives & Greenhouses: Converting processed poultry compost into premium organic fertilizer pellets for local vineyards, vegetable farms, and orchards.
3. Municipal Organic Co-Treatment: Co-fermenting poultry manure with urban green waste and food processing leftovers to maximize regional bio-energy efficiency.
Phase 1: Environmental Audit & Customization: Analyzing local moisture, C:N ratios, and facility layout in Skopje for bespoke equipment configuration.
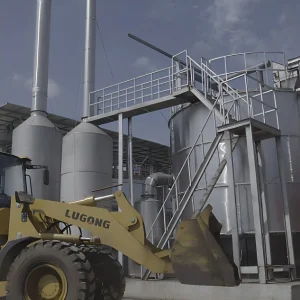
Phase 2: Automated Deployment & Integration: Installation of intelligent fermentation tanks equipped with remote IoT monitoring and automated aeration control.
Phase 3: Long-term Compliance & Support: Ongoing spare parts supply, firmware updates, and agronomic advisory services to ensure maximized fertilizer yield.
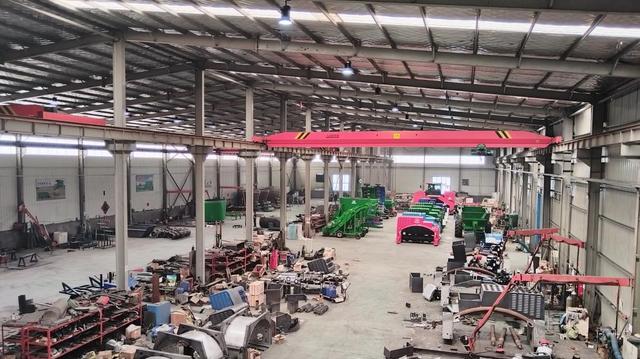
Chengdu AgBio Energy Co., Ltd. is a professional manufacturer specializing in organic waste composting equipment, food waste recycling systems, and sustainable waste treatment solutions. Established in 2013 and headquartered in Chengdu, Sichuan Province, China, the company is dedicated to helping businesses, agricultural operations, municipalities, and environmental service providers transform organic waste into valuable resources. With a modern manufacturing facility covering more than 16,000 square meters and a team of over 230 employees, AgBio Energy delivers efficient and environmentally responsible waste management technologies to customers around the world.
The company's product portfolio includes organic waste composting machines, food waste treatment systems, aerobic fermentation equipment, agricultural waste recycling solutions, manure composting systems, organic fertilizer production lines, municipal bio-waste treatment equipment, and intelligent composting management systems. These solutions are widely used in farms, food processing facilities, restaurants, hotels, commercial waste treatment centers, agricultural cooperatives, and municipal environmental projects.
AgBio Energy integrates engineering expertise, process optimization, and advanced manufacturing technologies to develop reliable composting and organic waste recycling systems. The company operates modern production workshops, assembly lines, and testing facilities to ensure product quality, operational efficiency, and long-term reliability. Strict quality management procedures are implemented throughout product development, manufacturing, installation, and customer support processes.
In addition to standard equipment, AgBio Energy offers OEM and ODM services, providing customized waste treatment solutions tailored to specific project requirements, processing capacities, and operational environments. The company works closely with environmental organizations, agricultural enterprises, waste management operators, and project contractors worldwide.
Committed to innovation, sustainability, and resource recovery, Chengdu AgBio Energy Co., Ltd. continues to support global efforts toward circular economy development, landfill reduction, and environmentally responsible organic waste management through advanced composting and recycling technologies.
Expert insights addressing technical, logistical, and compliance considerations for importing poultry waste composting machinery into Skopje.
Our intelligent aerobic fermentation tanks feature insulated dual-layer walls and automated temperature regulation systems. Even during cold Skopje winters, internal thermophilic bacteria activity is maintained at optimal levels (55°C–70°C), ensuring year-round continuous composting without performance degradation.
All equipment produced by Chengdu AgBio Energy adheres to strict international quality standards, holding CE certifications and ISO9001 quality management accreditations. They fully comply with biosecurity protocols for animal byproduct treatment and environmental emission limits.
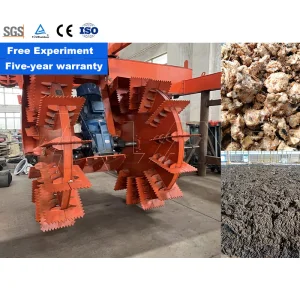
Utilizing our high-efficiency dynamic aerobic fermentation technology, the entire decomposition and deodorization cycle is completed within 7 to 10 days, converting raw slurry or litter into stable, nutrient-rich organic fertilizer ready for packaging or field application.
Yes. We provide comprehensive turnkey services including detailed installation blueprints, remote video engineering guidance, and—upon request—on-site engineer dispatch for physical installation, operational testing, and staff training.
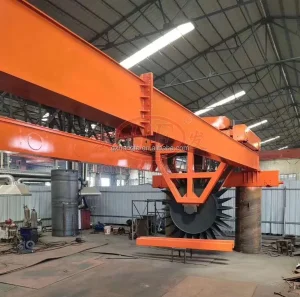
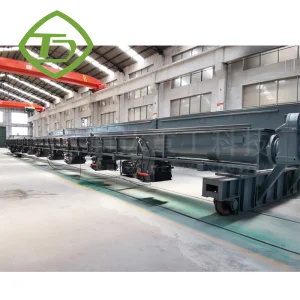
Explore our full catalog of specialized turners, fermentation tanks, mixers, and automated fertilizer packaging systems.
Contact our engineering team today for customized quotations, technical specifications, and expert consultation tailored to your project capacity.
Send Inquiry Now AgBio Energy